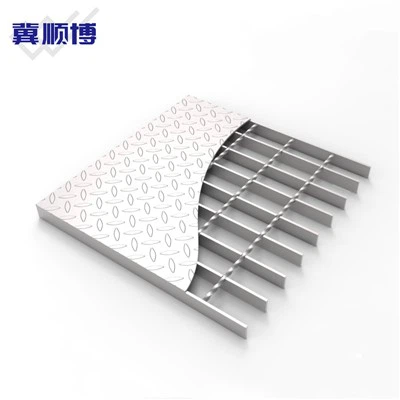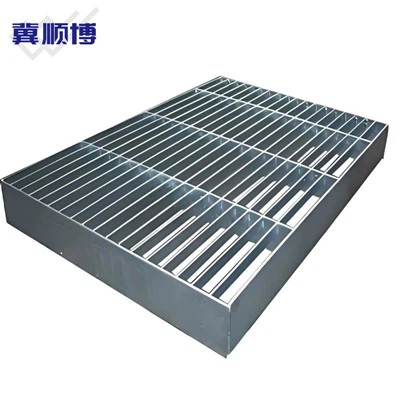
Hot-dip galvanizing looks like a finishing step, but the order of work matters. In our workshop, a grating panel is cut, welded, banded, and checked before it goes for zinc treatment. If a corner, hole, or removable section is added afterward, fresh steel is exposed again. That means touch-up work and a less tidy job.
For galvanized steel grating, the zinc layer is mainly there to slow corrosion when rain, wash water, or damp plant air reaches the steel. We offer hot-dip galvanizing as the regular treatment for this grating range, with electro-galvanizing available as an alternative finish. We choose the finish after the service environment is clear. The drawing still comes first.
Span, bearing-bar size, spacing, edge bands, and cut-outs need to be settled before coating. A serrated surface may be useful on wet walking areas, but it does not change the basic load calculation. Galvanizing does not make an undersized panel stronger. One practical habit helps: keep fabrication notes and finish notes on the same drawing.
When galvanized steel grating is ordered this way, our production team can check the panel as one job instead of chasing separate instructions. It also gives the buyer a cleaner basis for quotation, inspection, and installation later. That is simpler for everyone, especially when several panel sizes share one project and delivery.